
You lift a fresh print off the bed, and there it is. A web of thin, wispy threads stretched across every gap, as a spider moved in overnight.
It’s a familiar little sigh of “so close.” The print itself came out fine, but the cleanup ahead is annoying. The good news is that learning how to stop stringing on 3D printer parts is easier than those threads make it look.
Most stringing traces back to a handful of settings, not a broken machine. A few careful tweaks usually clear it up for good.
In this guide, I’ll walk you through what stringing actually is and why it shows up. Then we’ll get into the tools worth having and a step-by-step process to fix it. By the end, you should be pulling clean prints off the bed with almost no cleanup.
What Causes Stringing on a 3D Printer
Before you start changing settings at random, it helps to understand where those threads come from. Stringing isn’t mysterious once you know the mechanics.
Nearly every case boils down to one of four causes. Sometimes two of them team up.
Oozing During Travel Moves
Here’s the root of it. When the printhead jumps between two separate areas, the nozzle is still full of hot, melted filament.
That molten plastic wants to leak out. As the head travels across an open gap, a little seeps from the tip and stretches into a thin strand behind it. Multiply that by hundreds of travel moves, and you get a print draped in threads.
Temperature Set Too High
Heat plays a big role here. A nozzle running hotter than it needs to keeps the filament runny and eager to flow.
Runny filament drips more readily during those travel moves. Drop the temperature a bit, and the plastic firms up just enough to stay put. It’s often the single most effective change you can make.
Poor or Insufficient Retraction
Retraction is the printer’s built-in defense against oozing. It pulls filament back slightly before a travel move, relieving pressure at the nozzle.
When retraction is weak, disabled, or badly tuned, that pressure stays. So filament keeps seeping out during travel. Dialing this in properly solves a large share of stringing problems.
Wet or Low-Quality Filament
This one catches people off guard constantly. Filament absorbs moisture from the air, and damp filament misbehaves.
When wet plastic hits the hot nozzle, the trapped water turns to steam and sputters. That sizzling causes extra oozing and stringing no setting can fully fix. A soggy spool is a surprisingly common hidden culprit.
Understanding the Types of Stringing
Not all stringing looks the same, and the differences tell you something useful. Take a moment to look closely before you start adjusting.
What you see points you toward the likely cause. That saves you from guessing blindly.
Fine Hair-Like Wisps
These are the light, thin strands that brush away with a finger. They’re barely there, honestly.
Fine wisps usually mean your settings are close, just not quite dialed in. A small temperature drop or a minor retraction tweak often clears them entirely.
Thick, Stubborn Strands
Heavier threads are a different story. When the strands feel substantial and cling hard, something bigger is off.
Thick stringing typically points to a nozzle that’s too hot or retraction that’s badly tuned or missing. These take more than a nudge to fix, but they’re still very solvable.
Blobs and Zits Alongside Stringing
Sometimes you’ll notice small bumps on the surface right alongside the threads. Those little zits often travel with stringing.
The reassuring part is that they usually share the same causes. Fix the temperature and retraction for the stringing, and the blobs tend to clear up too.
Tools and Materials You Will Need
The nice thing about this fix is how little it demands. You probably have most of what you need already.
A few basics will carry you through the whole process without any special purchases.
A Stringing Test Model
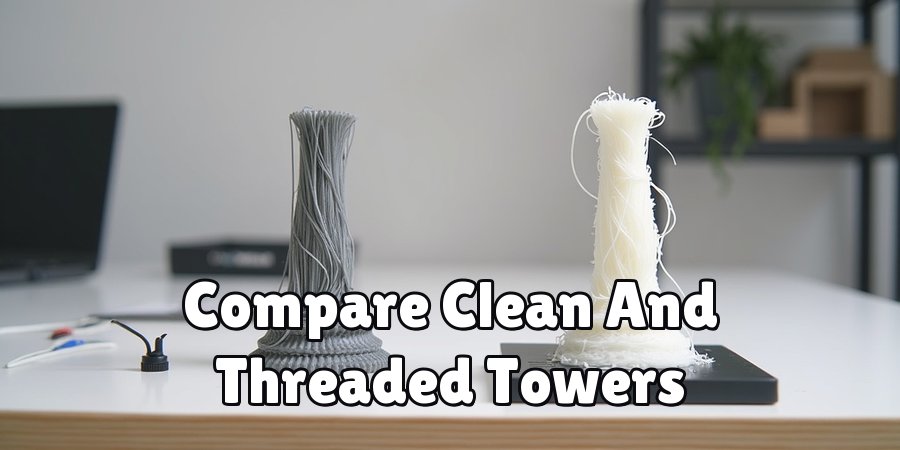
This is your measuring stick. A simple two-tower test print, or a comb-style model, instantly shows whether your changes are working.
The idea is that the printhead has to travel back and forth across a gap repeatedly. Any stringing shows up plainly in that open space, so you can compare before and after at a glance.
Slicer Software Access
Most of the real tuning happens in your slicer. Cura, PrusaSlicer, and Bambu Studio all put retraction, temperature, and travel settings within easy reach.
You don’t need anything fancy here. Whatever slicer you already use will have the controls this guide covers.
A Filament Dryer or Storage Solution
Since moisture is such a common cause, a way to dry filament helps enormously. A dedicated dryer box is ideal.
If you don’t have one, a sealed container with desiccant keeps spools dry between prints. Some people even use a low oven for drying, carefully. Either way, keeping moisture out prevents a whole category of stringing.
How to Stop Stringing on 3D Printer: Step-by-Step Guide
Here’s the heart of it. Work through these seven steps in order, and change just one thing at a time. That single habit is what turns troubleshooting into something reliable rather than a shot in the dark.
Print your test model after each change. It’s the only honest way to see what actually helped.
Step 1: Dry Your Filament First
Start here, always. Dry your spool in a filament dryer, a dedicated box, or a low oven before you touch any settings.
Wet filament causes stringing that no amount of tuning can cure. So there’s no point chasing temperature and retraction until you’ve ruled moisture out. This step alone sometimes solves the whole problem.
Step 2: Lower Your Printing Temperature
Now drop your nozzle temperature in small steps, around 5 degrees at a time. Print your test tower after each drop.
A cooler nozzle keeps the filament firmer, so it oozes far less during travel. Keep lowering until you find the point where stringing fades, but the layers still bond well. Go too far, and you’ll see under-extrusion, so watch for that balance.
Step 3: Enable and Tune Retraction Distance
If retraction is off, turn it on. Then adjust the distance, which controls how far filament pulls back before a travel move.
This setting depends heavily on your printer type. Bowden setups, with their long tube between extruder and nozzle, need more distance. Direct-drive machines need much less. Start with your printer’s recommended value and test from there.
Step 4: Adjust Retraction Speed
Distance is only half of retraction. Speed matters too, and it’s about how fast the filament gets pulled back.
Aim for a quick, clean pull that clears the pressure at the nozzle before the head moves. Too slow, and oozing sneaks through anyway. Too fast, and you risk grinding the filament. Adjust in small increments and check the result each time.
Step 5: Increase Travel Speed
Here’s a simpler lever. Speed up your travel moves so the printhead crosses gaps faster.
The logic is straightforward. The less time the nozzle spends hovering over open space, the less chance any oozing plastic has to stretch into a strand. Quicker hops between areas naturally reduce stringing.
Step 6: Enable Combing and Wipe Settings
Combing keeps travel paths inside the printed area instead of crossing open gaps. That way, any small ooze lands on the model rather than in visible space.
Wipe and coasting settings help too. They relieve nozzle pressure near the end of a move, so less plastic is sitting there ready to leak. Together, these features hide and shrink whatever stringing remains after your other tweaks.
Step 7: Run a Test Print and Refine
Finally, tie it all together. Print your stringing test one more time and study the result against your earlier attempts.
If threads still linger, adjust one setting and reprint. Patience wins here. Once the towers come out clean between them, note your winning values and lock them in. You’ve earned that clean print.
Best Practices for String-Free Prints
A few habits turn a one-time fix into results you can count on. None of them take much effort, and they save you from re-solving the same problem later.
Mostly, they’re about staying organized and consistent.
Store Filament Properly
Since moisture causes so much stringing, protect your spools between prints. A sealed container with desiccant does the job nicely.
It’s a small habit that prevents a big headache. Filament left out in a humid room slowly absorbs water, and then even dialed-in settings start producing threads again.
Change One Setting at a Time
I keep coming back to this because it matters more than any single tweak. Adjust one thing, then reprint and observe.
When you change several settings at once, and the print improves, you’ve learned nothing about which one helped. Isolating each change turns guesswork into something closer to a real test.
Keep a Settings Profile Per Filament
Different filaments want different settings. Once you’ve dialed in a brand or material, save that profile.
Next time you load the same spool, you skip the whole tuning process. It feels like overkill until the day it saves you twenty minutes and a pile of test prints.
Common Mistakes to Avoid
Everyone stumbles a little when they start fighting stringing. These are the missteps I see most, and each is easy to sidestep once you know it’s coming.
No judgment here. I’ve made all of them at some point.
Cranking Retraction Too High
When stringing persists, the temptation is to keep raising retraction. That often backfires.
Too much retraction can pull molten plastic away and cause clogs, grinding, or gaps in the print. More isn’t always better. Find the smallest distance that works, rather than the largest you can manage.
Ignoring Filament Moisture
This is the classic trap. People spend hours tweaking temperature and retraction while the real problem is a damp spool.
If you skip drying and nothing else seems to help, moisture is likely the answer. Dry the filament first, and a lot of frustrating troubleshooting simply disappears.
Changing Several Settings at Once
The urge to fix everything fast is understandable. It’s also counterproductive.
Stack three changes together, and you lose track of what actually made the difference. Worse, a good tweak can hide a bad one, leaving you confused. Slow down and isolate each change.
Tips to Prevent Stringing in the Future
Once your prints come out clean, a little upkeep keeps them that way. These small routines head off stringing before it returns.
They’re easy to fold into your normal printing habits.
Maintain a Clean Nozzle
Buildup inside or around the nozzle worsens oozing over time. A quick clean now and then keeps things flowing smoothly.
It’s the kind of maintenance that’s easy to forget until prints start looking rough. A clean nozzle simply behaves more predictably, which means less stringing.
Check Filament Quality Before Big Prints
New spool? Run a quick test print before committing to a long job.
That small check catches moisture or quality issues early, when they’re easy to deal with. Discovering a stringy spool after a twelve-hour print is a special kind of disappointment worth avoiding.
Revisit Settings Seasonally
Your perfect settings aren’t permanent. Humidity shifts with the seasons, and filament ages over time.
So it’s worth re-tuning now and then, especially if stringing creeps back after months of clean prints. A little seasonal adjustment keeps everything running the way you dialed it in.
Frequently Asked Questions
A few questions come up again and again once people start tackling stringing. Here are honest answers.
Why Does My Printer String With PETG?
PETG is simply prone to it. The material stays gooey and strings more readily than PLA does, which frustrates a lot of newcomers.
The fixes are the same, just applied more firmly. Dry the PETG thoroughly, use higher retraction, and lean toward slightly lower temperatures. It takes patience, but clean PETG prints are absolutely achievable.
Can Wet Filament Really Cause Stringing?
Absolutely, and it’s one of the top causes. Moisture trapped in the filament turns to steam at the nozzle and sputters out.
That sputtering creates oozing and stringing that settings alone can’t fully fix. Drying the spool often solves the problem almost instantly, which surprises people every time.
What Retraction Distance Should I Use?
It depends on your printer’s setup. Bowden systems, with that long tube, often need somewhere around 4 to 7mm.
Direct-drive machines need far less, usually about 0.5 to 2mm. These are starting points, not rules. Test from there and adjust based on what your stringing towers actually show you.
Conclusion
Learning how to stop stringing on 3D printer parts comes down to a handful of simple, repeatable adjustments. What looks like a messy, discouraging problem is usually just a few settings waiting to be dialed in.
The path is clear. Dry your filament first, lower the temperature, tune your retraction distance and speed, then speed up travel and enable combing to clean up the rest.
A few habits keep the results lasting. Change one setting at a time, store your filament properly, and save a profile for each material you use.
So start with dry filament and a small temperature drop, since those two moves deliver the fastest wins. Print a stringing test, make one change, and watch the threads disappear. There’s a genuine satisfaction in lifting a flawless, string-free print off the bed, knowing you tuned your machine to get it there.

About
Zevric Halden is a dedicated expert in the world of 3D printing, printer repair, and additive manufacturing, with years of hands-on experience troubleshooting, maintaining, and optimizing desktop 3D printers. His professional focus lies in combining practical mechanical knowledge with modern 3D printing technologies to help users solve printer problems, improve print quality, and keep their machines running reliably. As the author of 3DMend, Zevric explores the technical side of 3D printing, making complex printer issues easier to understand for makers, hobbyists, and professionals alike.
Education
Rochester Institute of Technology
(Rochester, New York, USA)
Associate Degree in Mechanical & Manufacturing Technology
- Focused on mechanical systems, manufacturing processes, machine maintenance, and precision tools.
- Developed practical experience with mechanical troubleshooting, electronic components, and computer-controlled equipment.
- Gained hands-on knowledge of CAD systems, rapid prototyping, and additive manufacturing technologies.
Worcester Polytechnic Institute
(Worcester, Massachusetts, USA)
Bachelor’s in Mechanical Engineering & Additive Manufacturing
- Specialized in digital fabrication, 3D printing systems, mechanical design, and manufacturing technologies.
- Studied printer calibration, motion systems, extrusion mechanisms, material behavior, and print optimization.
- Participated in practical engineering projects involving rapid prototyping, machine diagnostics, and 3D-printed components.
Publications and Impact
Through 3DMend, Zevric shares his expertise on 3D printer troubleshooting, maintenance, calibration, hardware repair, print-quality issues, and additive manufacturing. His writing focuses on turning frustrating printer problems into clear, practical solutions that readers can understand and apply.
From nozzle clogs and extrusion problems to bed-leveling issues, calibration errors, overheating, unusual noises, failed prints, and mechanical wear, Zevric’s guides are designed to help users identify the underlying cause rather than simply treating the symptoms.
His work bridges the gap between technical engineering knowledge and everyday 3D printing, making reliable repair and maintenance information accessible to everyone—from first-time 3D printer owners and hobbyists to experienced makers and professionals.